Stamping Metal Part for OEM and Suppliers | Precision Stamping
I craft stamping metal part solutions that meet tight tolerances and demanding budgets. I work closely with {OEM} teams and {Suppliers} to ensure every order aligns with your production schedule. From prototype stamping to high-volume runs, my process guarantees repeatable precision, clean edges, and minimal spring-back. I source compatible alloys and coatings, select tooling that minimizes wear, and optimize stripping and deburring for assembly-ready parts. Lead times are shortened by integrated planning, on-site inspection, and first-pass quality checks at each stage. I can tailor sheet thickness, hole patterns, and stamping sequences to fit your assembly line, with traceability from raw sheet to finished part. If you seek reliable supplier performance and consistent quality for stamping metal part components, I’m here to help you scale efficiently and reduce total cost of ownership.


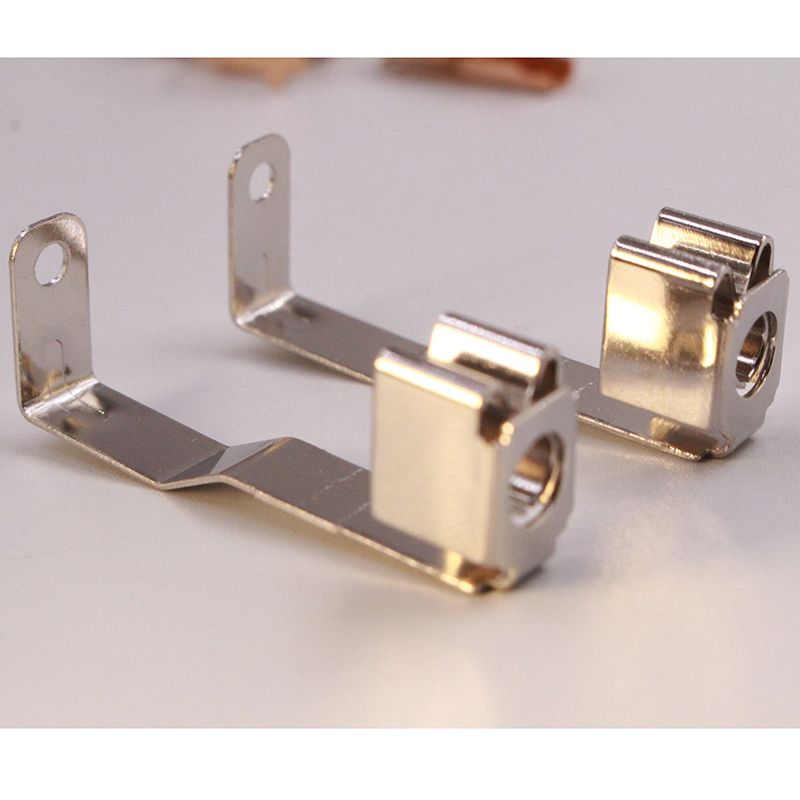
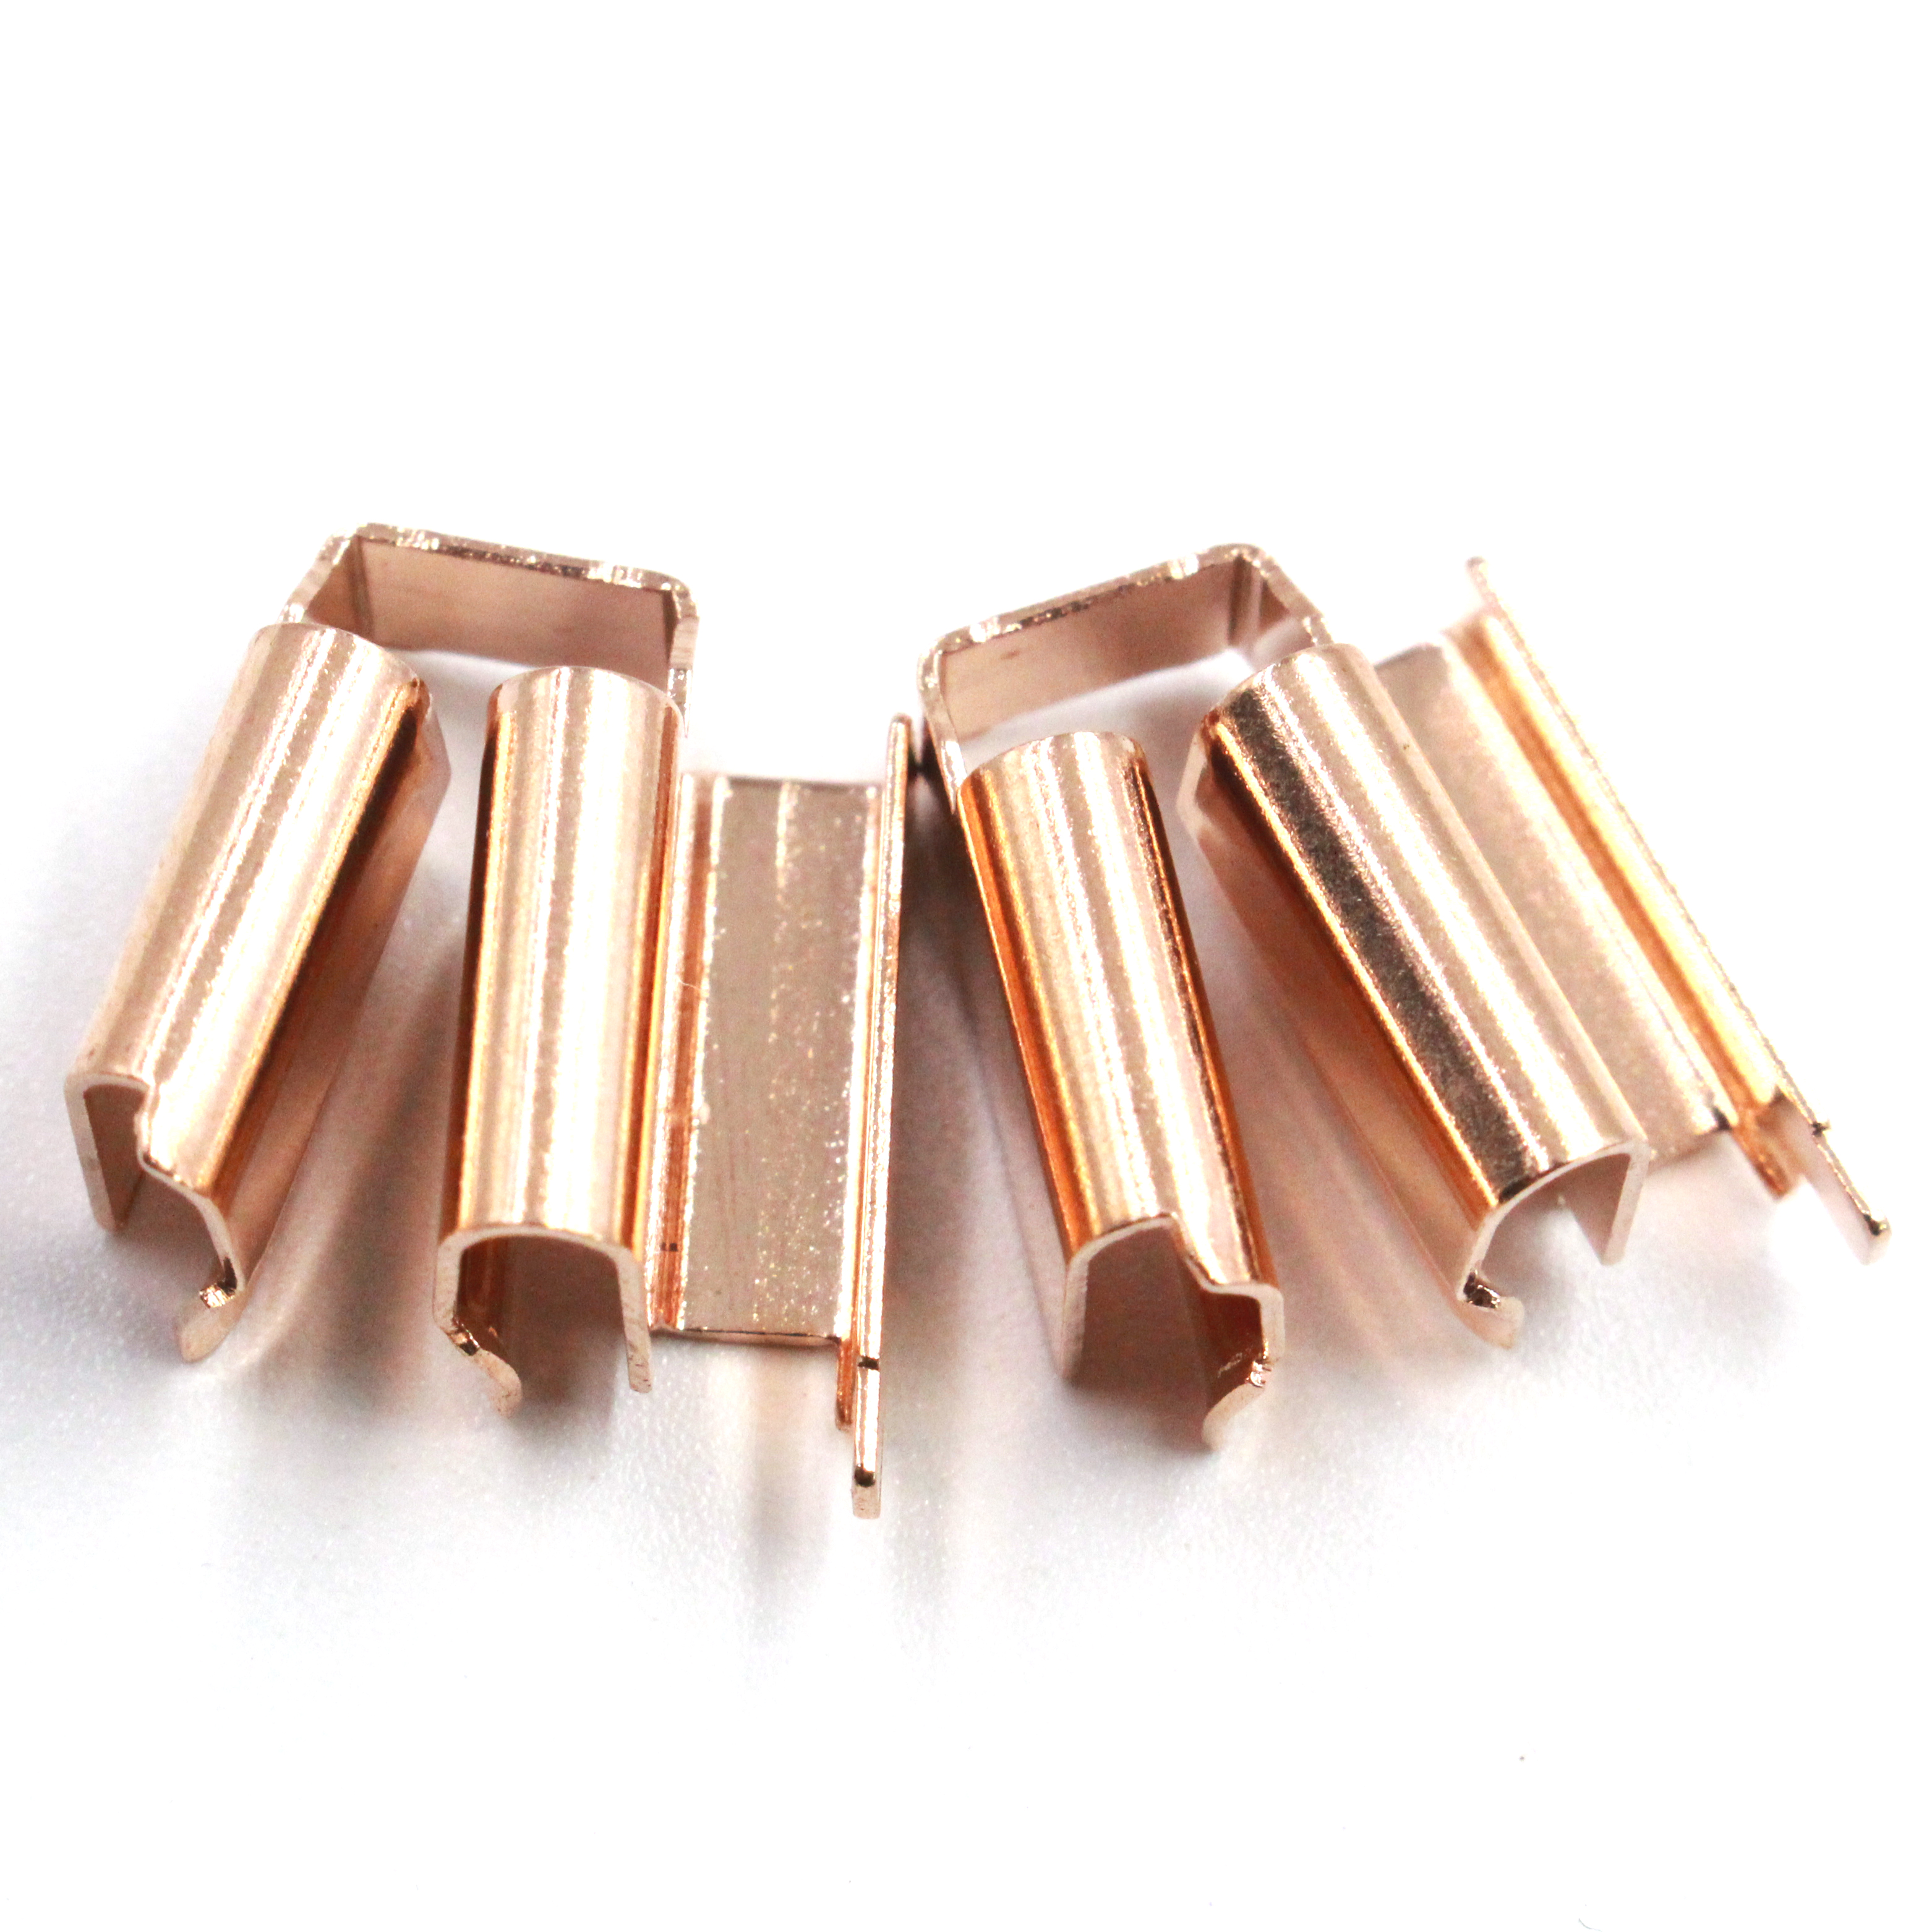
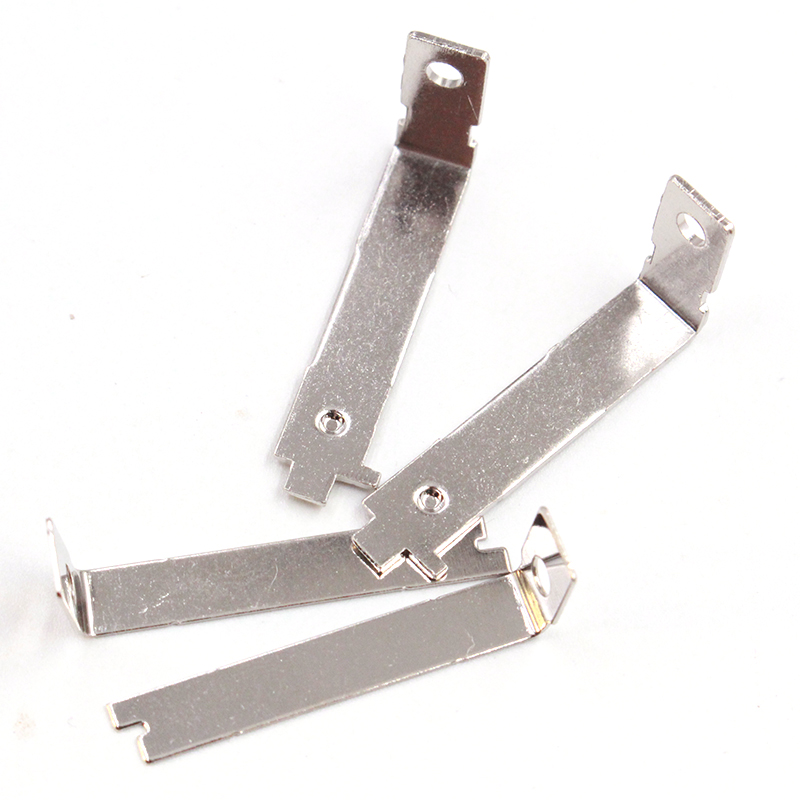

stamping metal part Ahead of the Curve Your End-to-End Solution
Global buyers in automotive, electronics, and industrial sectors seek stamping partners who can turn design into dependable metal parts quickly and consistently. Ahead-of-the-curve stamping blends material expertise, precision tooling, and multi-step processes with integrated finishing and assembly. By validating manufacturability early, using automation and real-time inspection, we can deliver tight tolerances, complex geometries, and high volumes while reducing waste and downtime. The result is parts you can trust across geographic markets and demanding applications. An end-to-end solution means more than parts: it means supply chain resilience. From rapid prototyping to scalable production, you get a single point of contact, streamlined logistics, and transparent quality data that trace every lot. With consistent process controls and continuous improvements, this approach lowers total cost, shortens lead times, and keeps critical programs on track for global procurement teams.
| Stage | Description | Cycle Time (s) | Throughput (parts/hour) | Yield (%) | Scrap (%) | Material | Energy per part (kWh) | Tool Life (cycles) | Equipment |
|---|---|---|---|---|---|---|---|---|---|
| Material Preparation | Prepare and feed raw stock to line | 10 | 360 | 99.5 | 0.5 | Aluminum 6061 | 0.08 | 150,000 | Reel-fed stock preparation line |
| Cutting & Blanking | Blanking of sheets to required blanks | 12 | 300 | 99.3 | 0.7 | Aluminum 6061 | 0.12 | 120,000 | Precision blanking press (1000 t) |
| Piercing & Stamping | Stamped features and holes | 8 | 450 | 99.6 | 0.4 | Aluminum 6061 | 0.09 | 130,000 | Progressive stamping press |
| Forming | Deep drawing and shape forming | 15 | 240 | 99.2 | 0.8 | Aluminum 6061 | 0.15 | 110,000 | Draw/forming press |
| Trimming & Edge Deburring | Trim excess and deburr edges | 6 | 600 | 99.4 | 0.6 | Aluminum 6061 | 0.07 | 140,000 | Chamfer/deburr die |
| Deburring & Cleaning | Final deburr and cleaner wash | 5 | 720 | 99.7 | 0.3 | Aluminum 6061 | 0.05 | 160,000 | Deburr station |
| Surface Treatment | Anodizing or powder coating (optional) | 60 | 60 | 99.0 | 1.0 | Aluminum 6061 | 0.80 | 50,000 | Anodizing line |
| Assembly | Assemble subcomponents into final part | 20 | 180 | 98.9 | 1.1 | Finished components | 0.20 | 80,000 | Semi-automatic assembly cell |
| QA & Packaging | Final inspection and packaging | 8 | 450 | 99.5 | 0.5 | Finished product | 0.04 | 200,000 | QA station + packaging |
Related Products
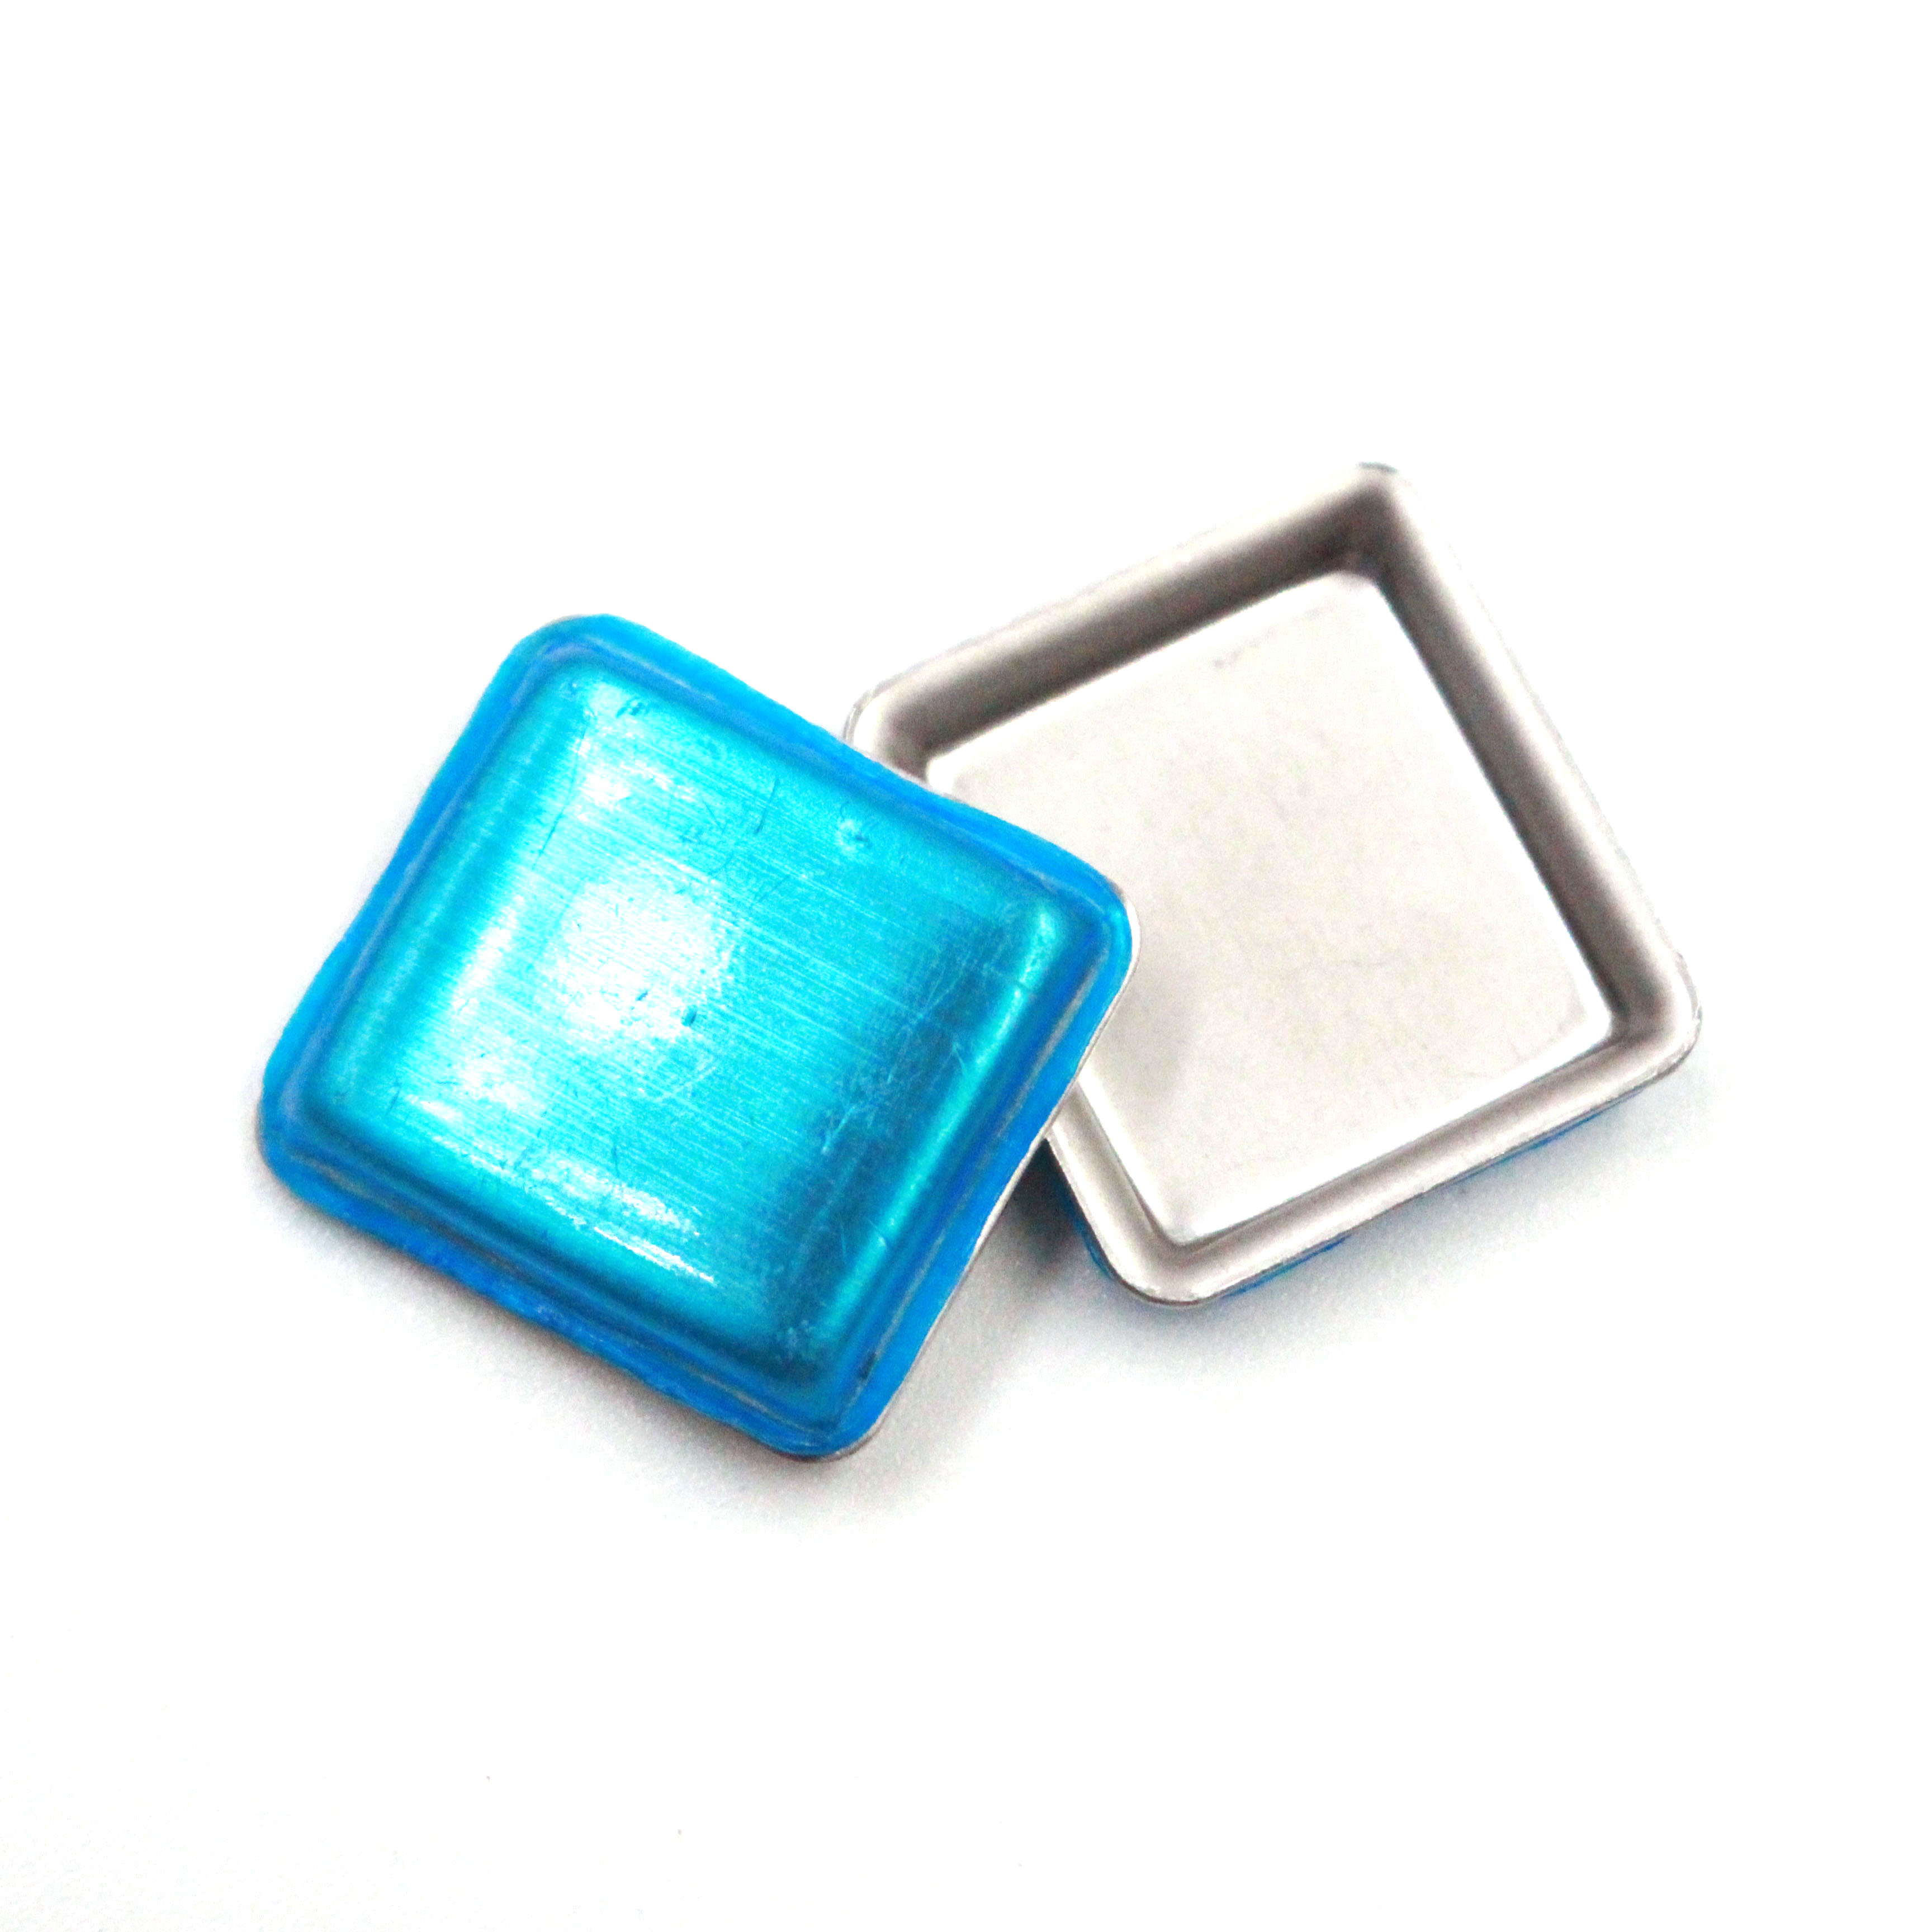


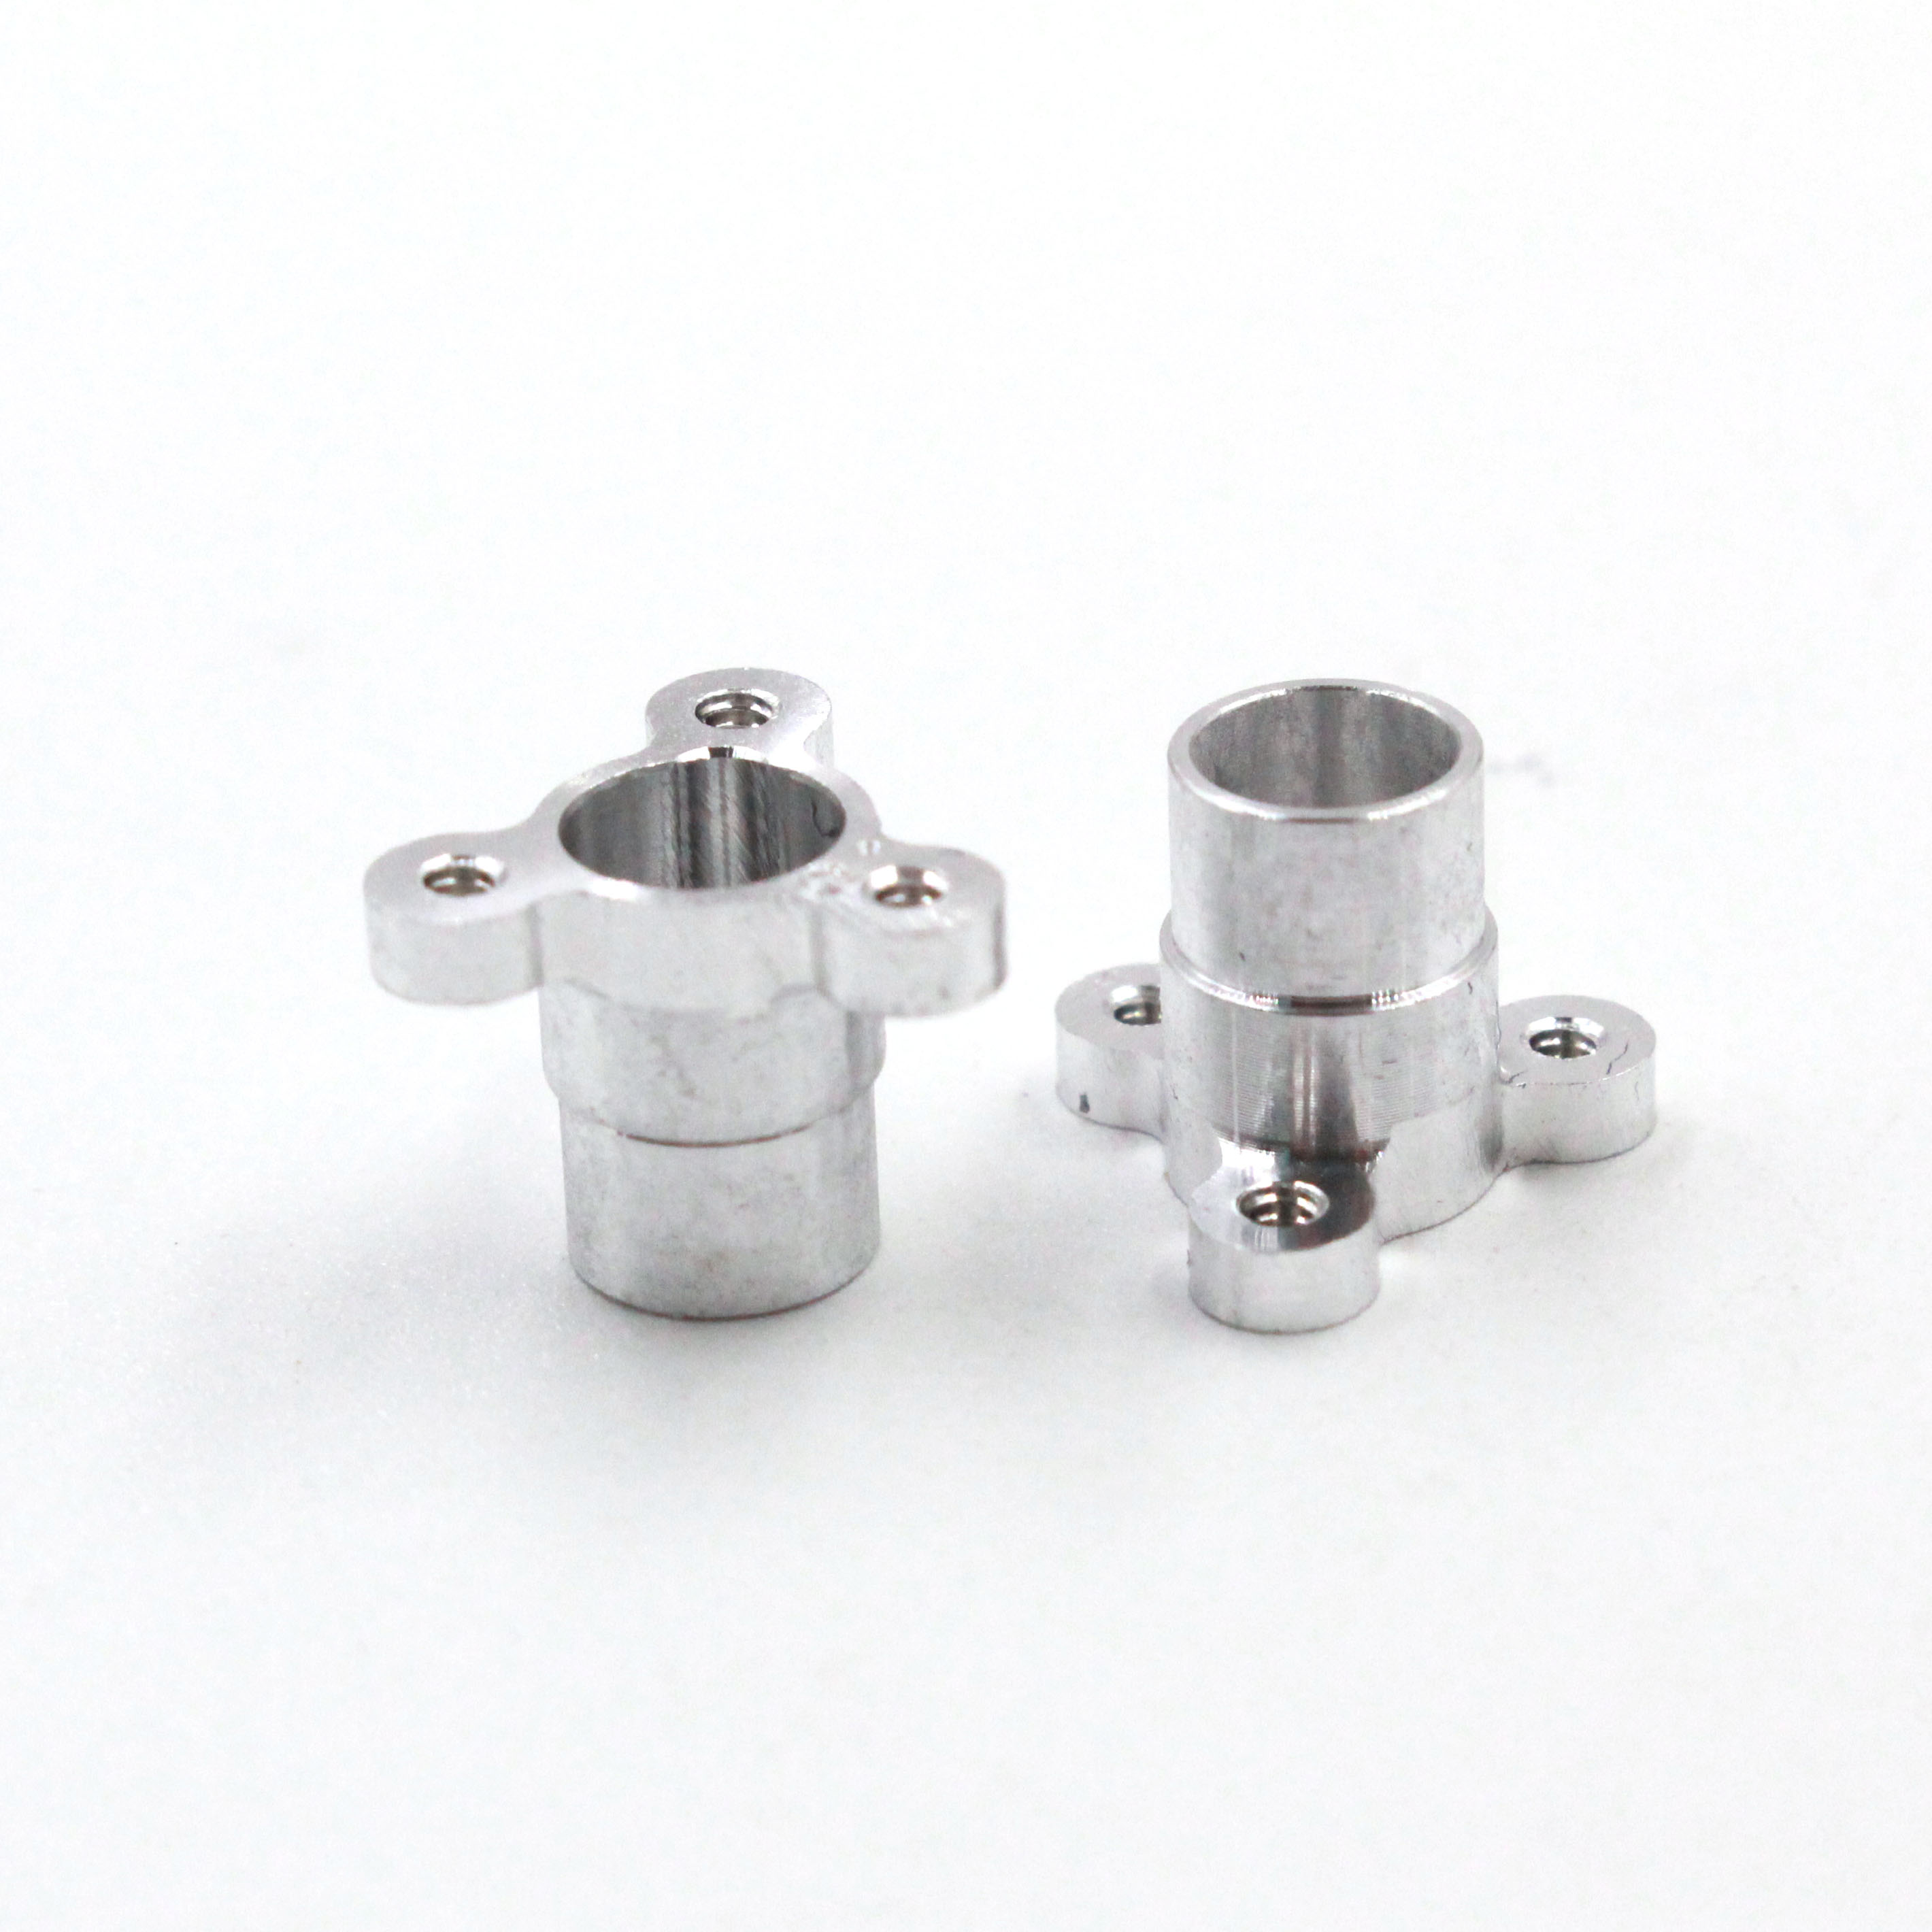


stamping metal part Manufacturer Factory
Top Selling Products

- Related Blog
- Reviews
- Reviews

-

Phone
-

E-mail
-

Whatsapp
-

WeChat
-

Top