CNC screw insert M3x4 - ODM Factory Solutions
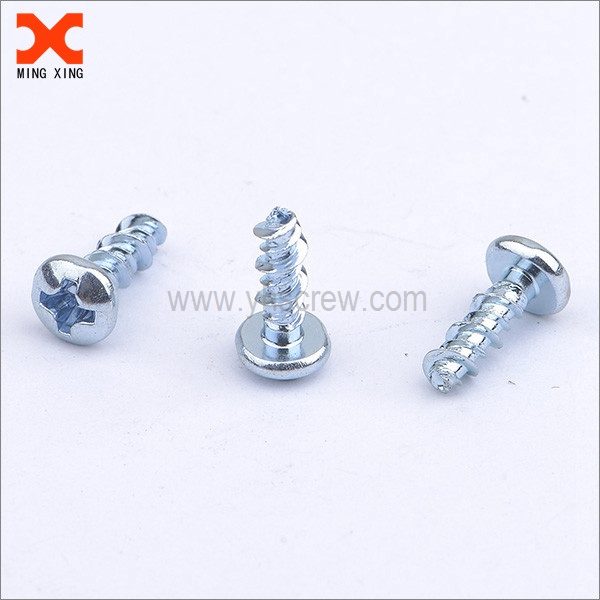
I’m a dedicated fastener producer delivering reliable {CNC screw insert M3x4} for metal and plastic assemblies. Each insert is machined with tight tolerances, then finished with corrosion-resistant plating for long life in demanding environments. I offer easy installtion with a self-centering drive and secure grip, so your assemblies stay precise through vibration and thermal cycles. For {ODM} ,{Factory} needs, I tailor counts, packaging, and documentation, including technical drawings and sampling, to fit your line. My team controls quality from raw material to final inspection, ensuring consistent inserts that mate perfectly with standard M3 threads. Shipping is prompt, with flexible MOQs and scalable production to support ramp-ups. If you want a partner who understands design-for-manufacture and cost-conscious sourcing, I’m here to align with your timeline and specs. Let me know your target tolerances and finish, and I’ll prepare a competitive quote for your next project.
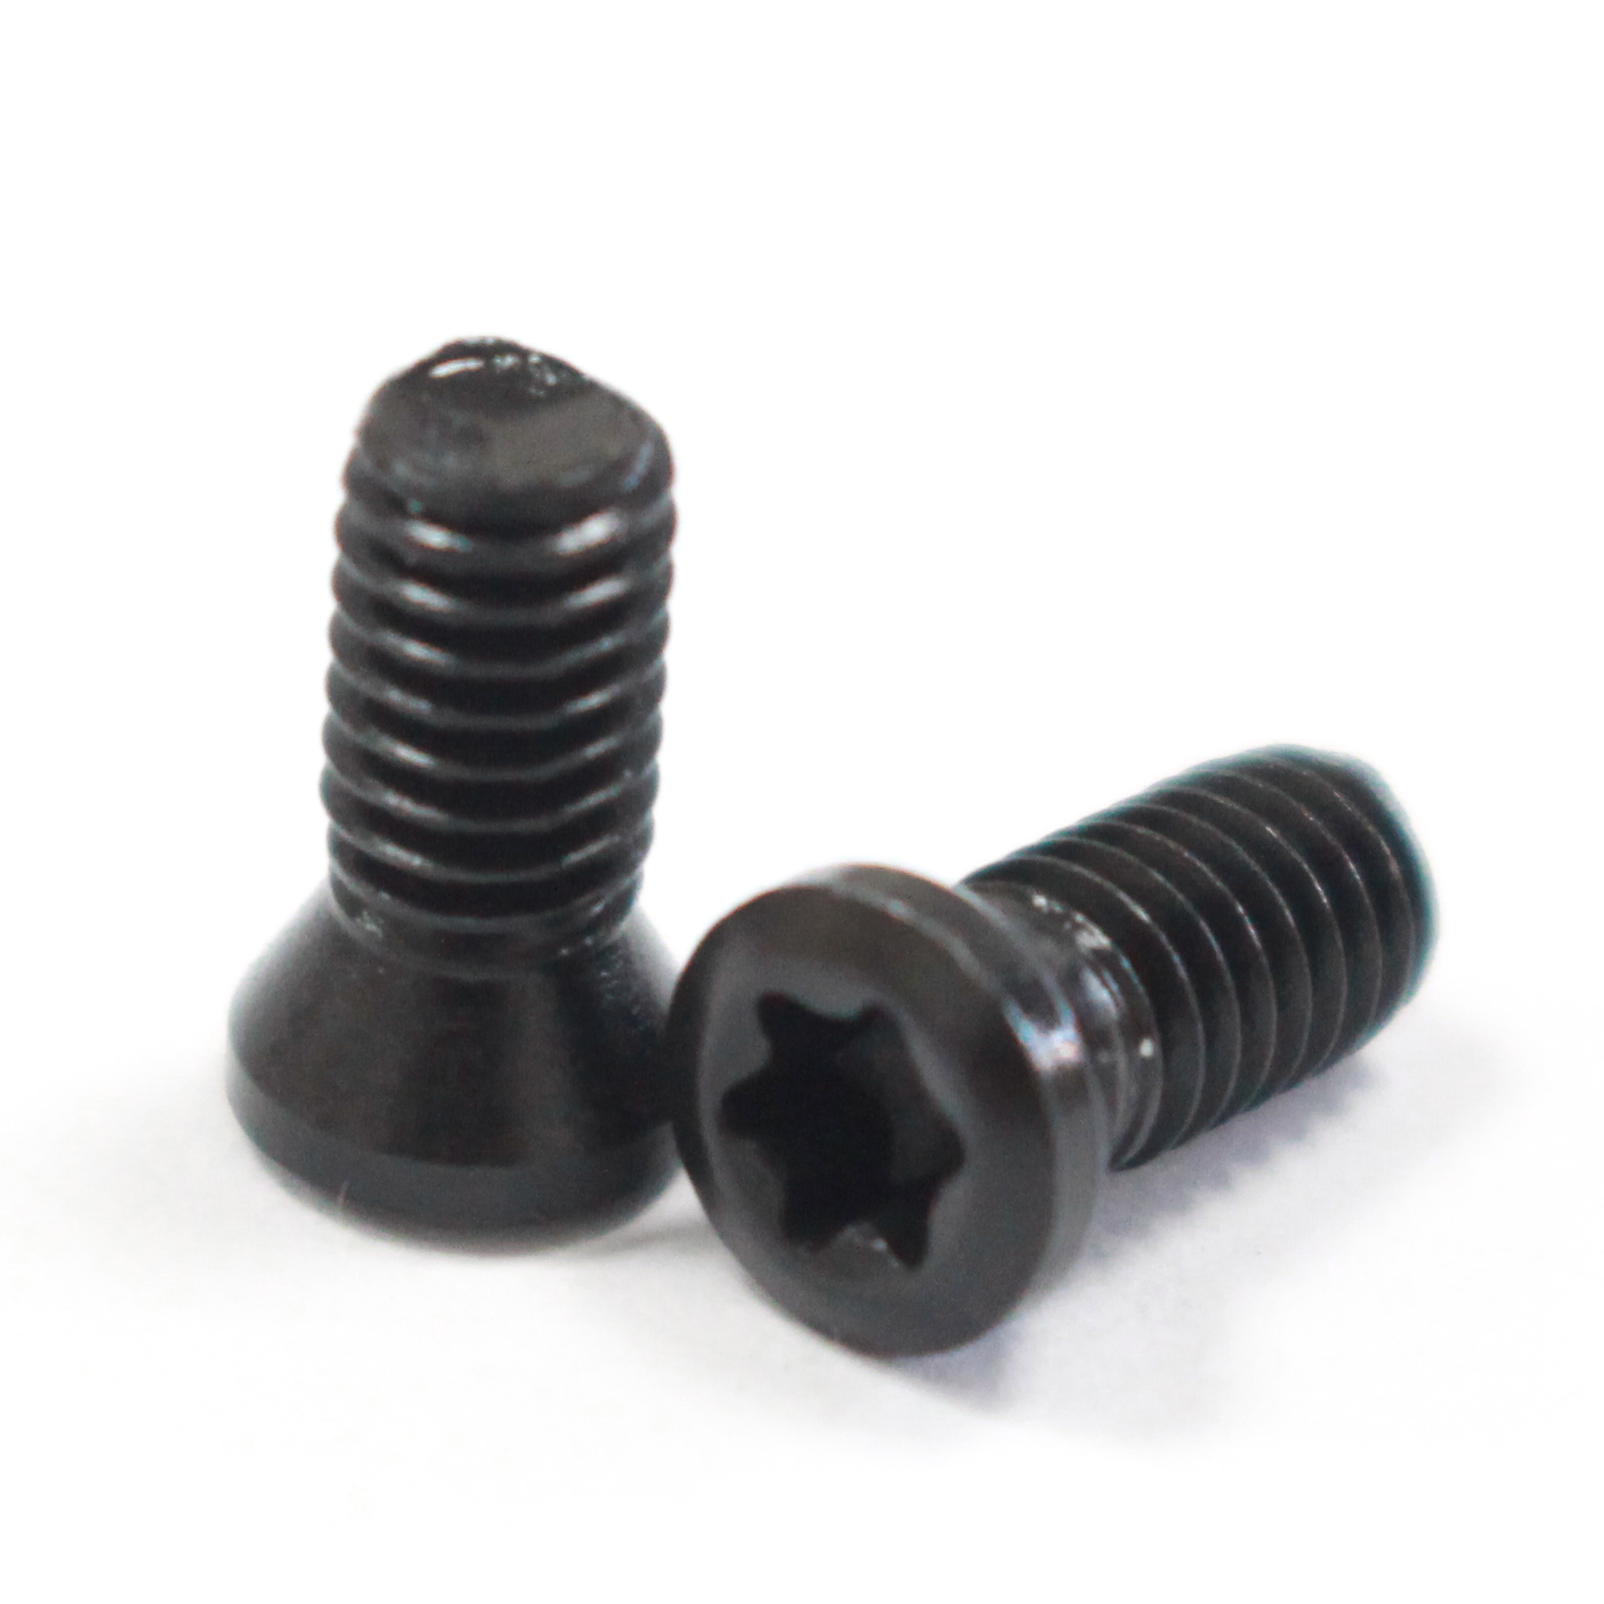
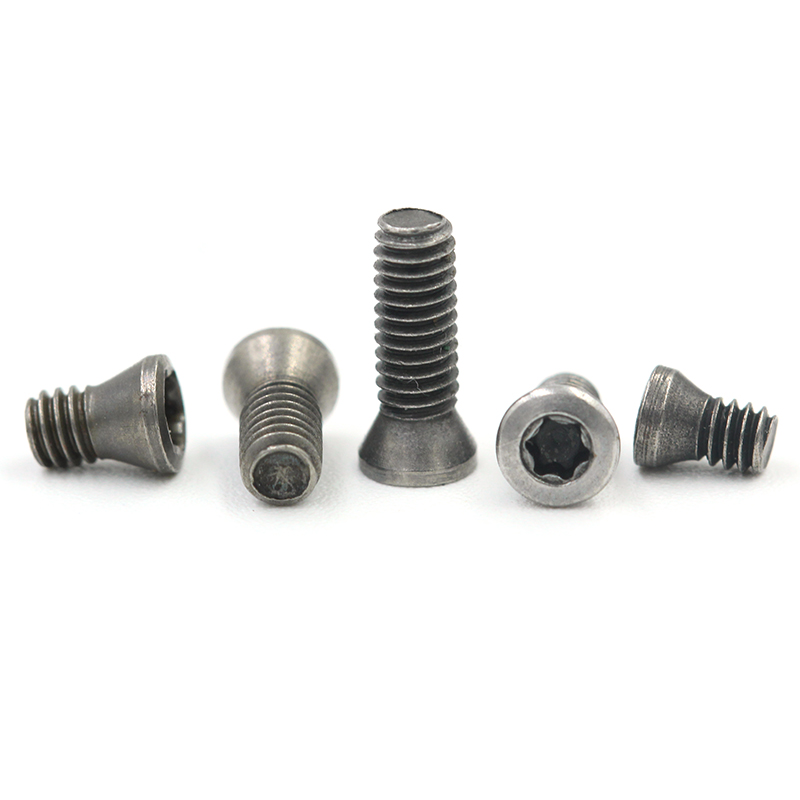
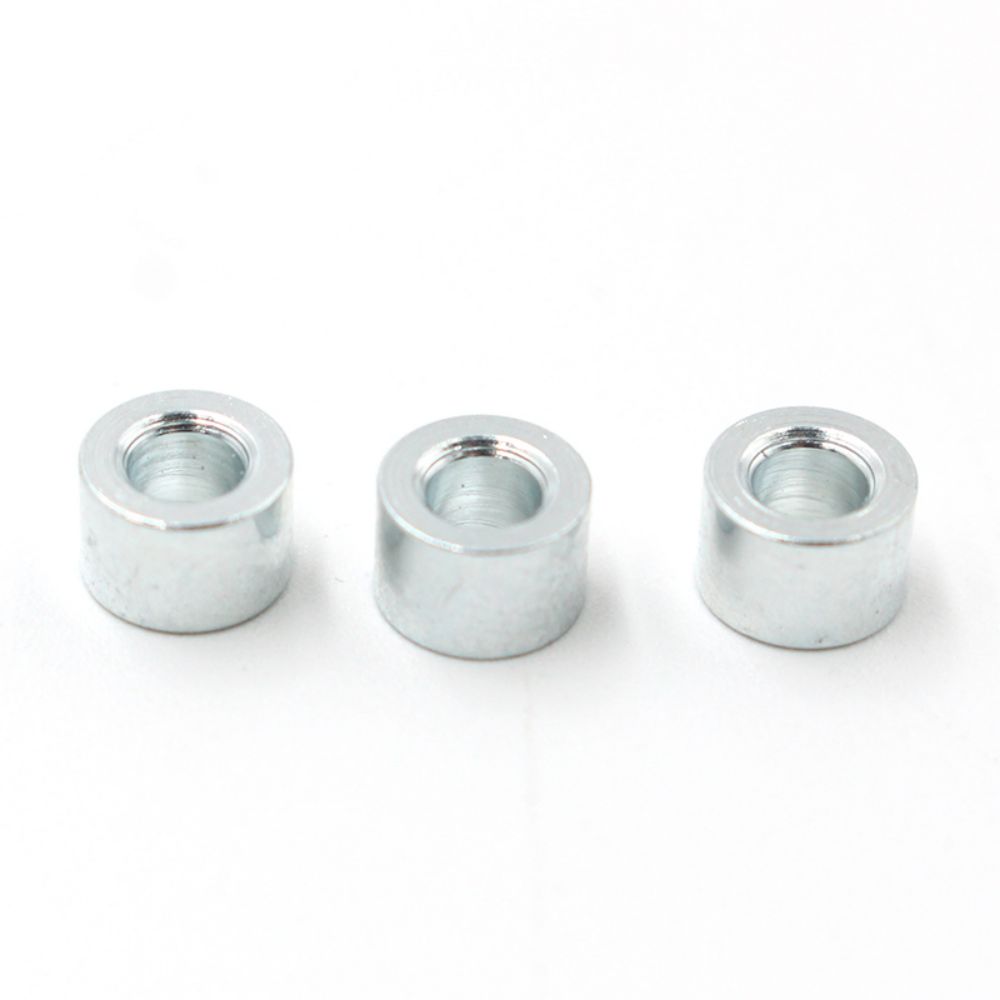


CNC screw insert M3x4 Dominates Sets the Industry Standard
Standardized CNC screw inserts in the M3x4 size are redefining plastics assemblies. Precision-machined to tight tolerances, they deliver consistent thread engagement, higher pull-out strength, and better vibration resistance. Their compact form fits slim housings and electronics, with reliable performance under heated insertion or press-in assembly. Buyers now treat this size as a global reference for interchangeable components, enabling streamlined sourcing and predictability across suppliers. The result is faster design cycles and lower assembly risk in consumer, automotive, and industrial applications. To leverage the standard, buyers should consider material (brass or stainless), finish, and installation method (hot-stake, press-in) that suits the polymer and equipment. Plan for supply stability, batch traceability, and compatibility with automation lines. Check tolerances, corrosion protection options, and packaging scales to support just-in-time manufacturing. By aligning with this industry standard, procurement becomes simpler, risk is reduced, and time-to-market for complex assemblies improves globally.
{ CNC screw insert M3x4 Dominates Sets the Industry Standard }
| Variant | Length (mm) | Material | Coating / Finish | Tensile Strength (MPa) | Shear Strength (kN) | Application |
|---|---|---|---|---|---|---|
| M3x4-SS304 | 4.0 | Stainless Steel 304 | Natural Passivation | 520 | 5.8 | General fastening in light-load applications |
| M3x4-SS316 | 4.0 | Stainless Steel 316 | Passivated (no coating) | 620 | 6.7 | Corrosive environments and marine use |
| M3x4-AL6061 | 4.0 | Aluminum 6061-T6 | Anodized | 310 | 2.2 | Lightweight assemblies |
| M3x4-CK45 | 4.0 | Carbon Steel CK45 | Black Oxide | 980 | 8.5 | High-load insert for metal-to-metal joints |
| M3x4-Brass | 4.0 | Brass (CuZn) | Natural finish | 280 | 1.4 | Non-magnetic and decorative uses |
| M3x4-NS-Nitrided | 4.0 | Alloy Steel with nitriding | Nitrided | 900 | 7.3 | Wear-resistant, heavy-duty applications |
Related Products



CNC screw insert M3x4 Ahead of the Curve Where Service Meets Innovation
Top Selling Products




- Related Blog
- Reviews
- Reviews

-

Phone
-

E-mail
-

Whatsapp
-

WeChat
-

Top